Keep supplied truck duty distinct from the treatment outcome
Confirm the deposit evidence, selected treating fluid and approved circulation assignment before choosing the heater, pump and connection package. The truck supplies its accepted heating and circulation functions; a product name or reference temperature does not establish removal of every blockage. Wax appearance temperature is fluid information, not a universal controller setting or proof of deposit dissolution.
Identify the actual onboard storage, indications and controls, external well or flowline equipment and return destination in the accepted offer. Collection and filtration do not automatically establish suitability for reuse. Keep well-program, material compatibility and site operating responsibilities with the competent project team. Do not assume universal scale, asphaltene or hydrate treatment, fixed cleaning time, restored production or unattended operation from a generic hot-oil truck description.
Start with the job decision
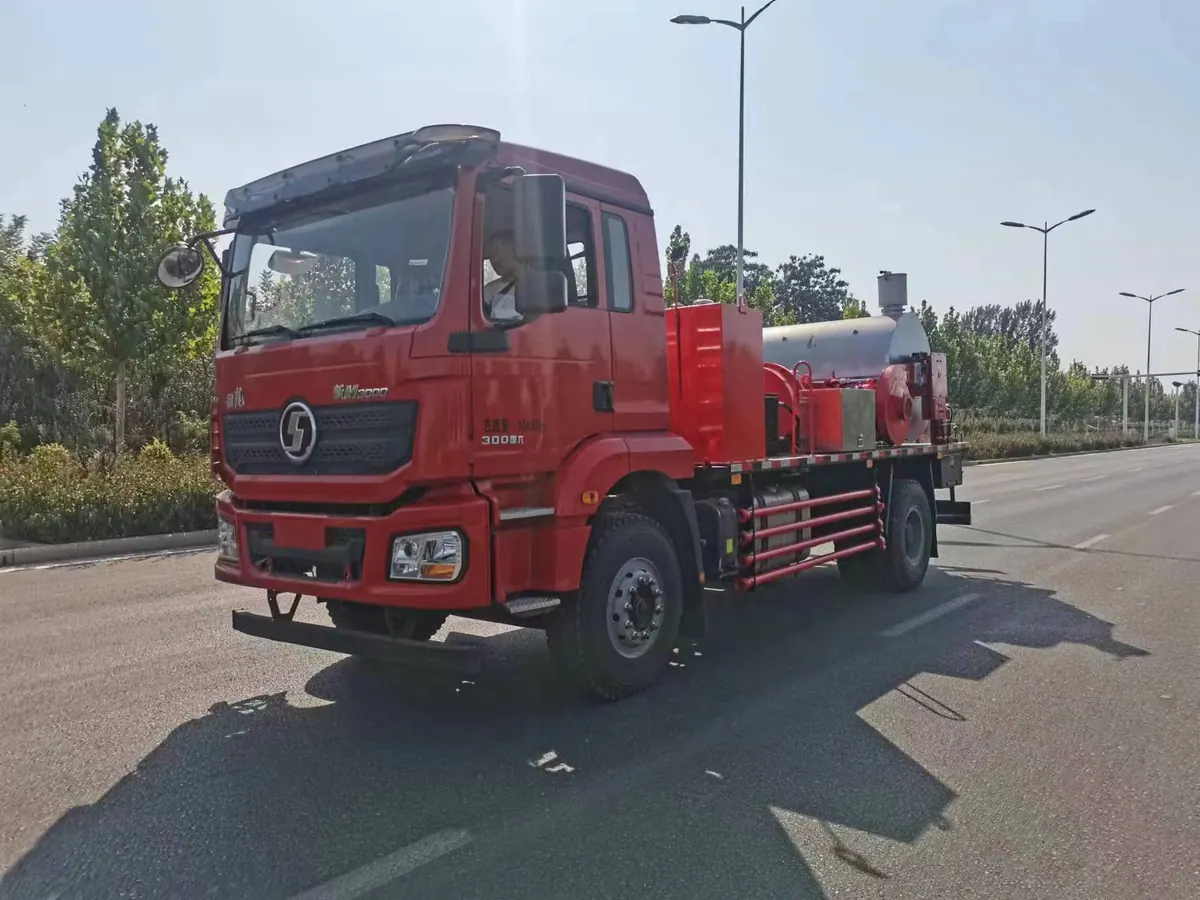
Oilfield Wax Removal Truck projects succeed when the equipment scope is tied to a defined operating duty: supplying controlled heating and circulation for an accepted paraffin-removal assignment. A useful project document separates normal duty, maximum credible duty, standby or transient conditions and the physical interfaces available at site. This keeps procurement language connected to field reality.
Record wax appearance temperature, deposit severity, target circulation temperature and pump pressure as ranges rather than isolated peak figures. The supplier can then explain how the hot-oil heater, circulation pump, specified fluid-storage and receiving arrangement and configuration-specific temperature, pressure and flame functions work together across the intended envelope.
Agree the FAT plan before manufacturing is complete
The inspection and test plan should identify hold points, witness points, acceptance criteria, required instruments and records. A FAT is not simply a visual factory visit. It should verify that the manufactured package matches approved documents and that controls and protection functions behave as agreed.
| Review item | What to confirm | Evidence or input |
|---|---|---|
| hot-oil heater | Accepted fluid, inlet condition, useful output and rate | Identified thermal boundary and evidence |
| circulation pump | Simultaneous heated pressure-flow duty and fluid restrictions | Configuration-specific selection response |
| specified fluid-storage and receiving arrangement | Actual tank roles, contents and return acceptance | Equipment and external supply schedule |
| configuration-specific temperature, pressure and flame functions | Indication, alarm and action scope identified separately | Accepted function and verification schedule |
Functional tests should follow the operating sequence
Test permissives, startup logic, normal control, alarms, controlled shutdown and emergency shutdown in a sequence that operators can recognize. Simulate relevant low, high and signal-failure conditions. If full-load testing is not practical at the factory, document the limitation and define the site acceptance test that will close it.
Do not release shipment with undocumented gaps
Compile signed test sheets, material and calibration records, final drawings, manuals, spare-parts lists, packing lists and the punch list. Classify open items by whether they prevent shipment, prevent installation or may be closed during commissioning. Photographs help, but they do not replace signed acceptance records.
Keep a usable project record
Maintain one controlled file containing the approved duty sheet, supplier clarifications, drawings, component data, inspection records, test results, deviations, photographs and signed acceptance documents. Record document revisions and the person responsible for each open item. This prevents the operating team from receiving a package whose final configuration differs from the information used during procurement.
The handover set should also identify installed component models, consumables, calibration intervals, recommended spares, preservation requirements and supplier support contacts. Capture baseline operating readings when the unit is accepted. Those records give maintenance personnel a reference for condition changes and allow later modifications to be reviewed against the original design basis.
Before closing the project, confirm that operators can find the startup, normal-operation, controlled-shutdown and emergency procedures relevant to their unit. Training attendance alone is not sufficient; the responsible team should demonstrate the required checks and know which conditions require escalation rather than continued operation.
Codes, standards and project requirements
Confirm the final specification and acceptance plan against the owner’s project standards, local jurisdiction and OSHA oil and gas extraction safety guidance. The applicable project documents govern whenever they are more specific.
Carry the agreed factory findings into the installation and commissioning review, keeping external interfaces, authorized site work and remaining acceptance evidence clearly assigned.